HICLOVER Waste Incinerators: Advanced Solutions for Global Waste Management Needs
Understanding HICLOVER Waste Incinerators: Engineering Reliability and Compliance
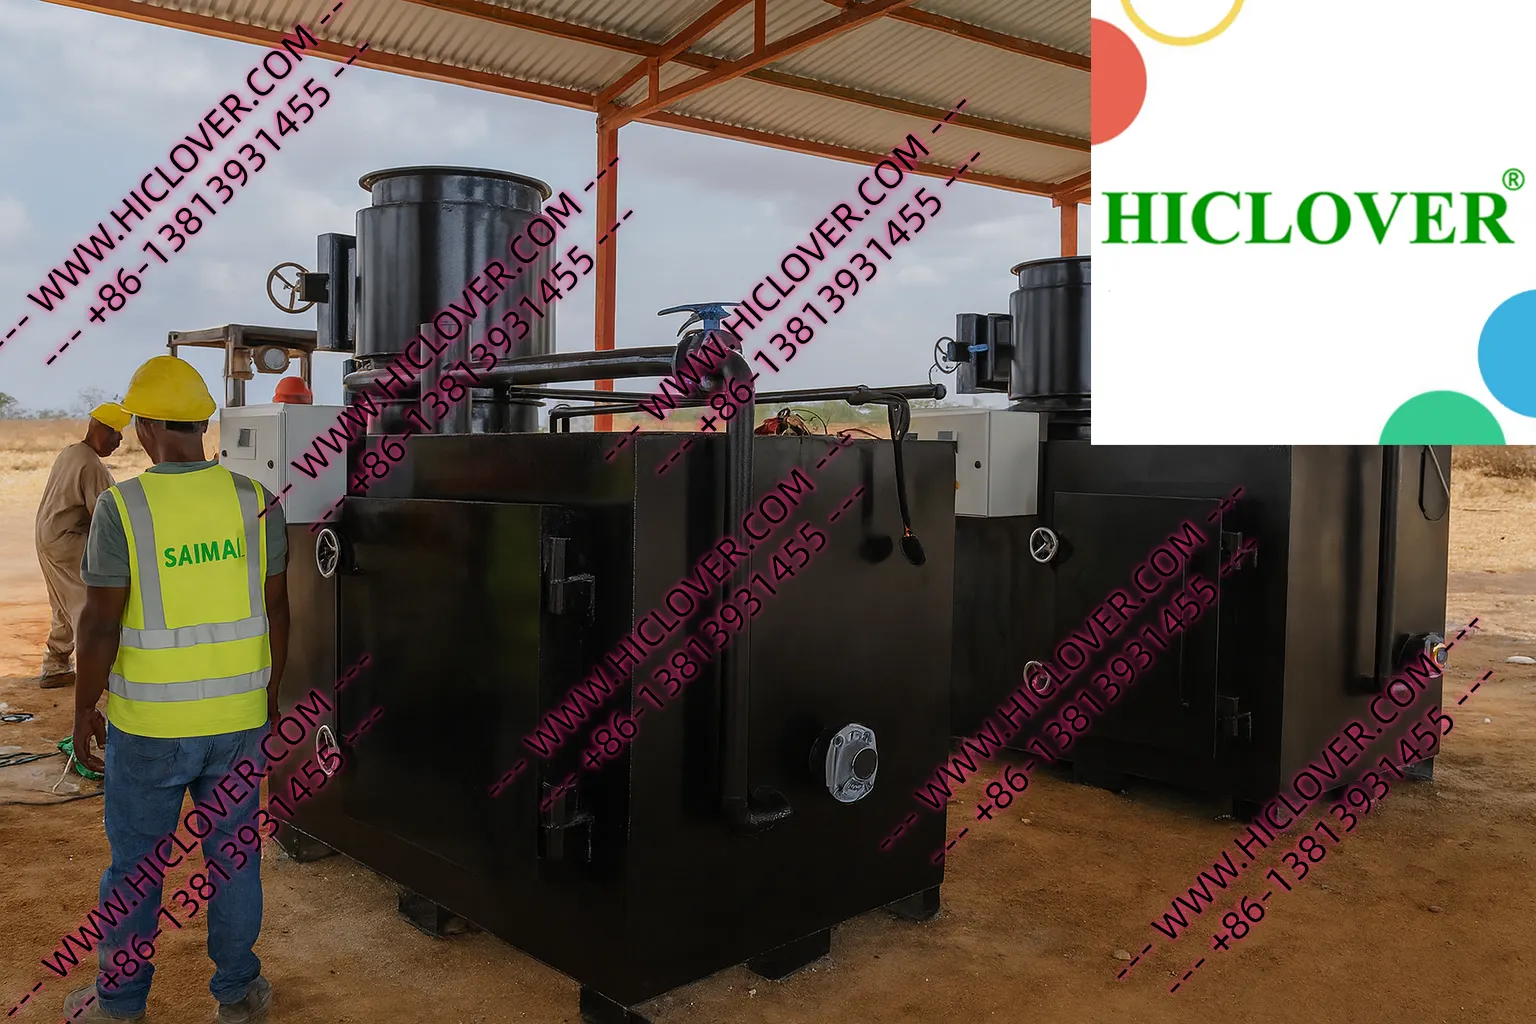
HICLOVER’s waste incinerators are engineered to meet the diverse needs of global waste management, including applications in Senegal bio waste incinerator, Liberia incineration, and Burundi incinerator suppliers. These systems are designed to comply with industrial standards and maintain a consistent operating temperature range for optimal performance. The integration of dual combustion chambers ensures thorough waste destruction, addressing the regulatory requirements set by WHO and EU emission frameworks. High-temperature retention is crucial for effective incineration, making HICLOVER an ideal choice for professional applications.
Technical Standards and Combustion Principles
HICLOVER waste incinerators are designed with technical precision, adhering to essential temperature standards for efficient combustion. These standards, indicated by medical incinerator operating temperature standards, ensure the effective breakdown of waste materials while minimizing emissions. The dual chamber system enhances combustion efficiency, maintaining high temperatures that are crucial for complete waste destruction. Compliance with stringent WHO and EU emission standards underscores the brand’s commitment to environmental responsibility and safety.
Comparative Analysis: Incinerator Types and Control Systems
Different types of incinerators are available to meet specific operational needs, such as fixed and containerized systems. HICLOVER offers both options, providing flexibility for various applications. The choice between PLC and manual control systems is another critical consideration. PLC automation offers streamlined operations and enhanced precision, ensuring consistency and safety in waste management processes. Mobile modular designs, like the Algeria portable incinerator, provide a plug-and-play solution suitable for remote site applications, such as crisis zones and humanitarian camps.
Environmental and Economic Considerations
HICLOVER’s commitment to sustainability is reflected in its waste management solutions, like the Gabon ecological incinerator. These systems are engineered to reduce carbon emissions, aligning with global pressures for carbon emission reduction and ESG compliance. The inclusion of energy recovery capabilities further enhances the economic viability of these systems, providing a dual benefit of waste destruction and energy generation.
Scrubber Options and Fuel Versatility
Customers can choose between wet and dry scrubbers, with each option offering unique advantages based on operational needs. The incinerators’ multi-fuel capability, supporting diesel, LPG, and natural gas, ensures adaptability to various fuel availability and cost considerations.
Global Reach and Customization
HICLOVER’s robust supply chain enables factory-direct supply and global export capability, ensuring a stable and reliable provision of incinerator systems. Customizable chamber volumes allow these systems to be tailored to specific waste management requirements, enhancing operational efficiency. With extensive engineering experience, HICLOVER offers solutions that cater to diverse applications, from Mozambique 3 kg per hour-incinerator systems to paper incinerators in industrial settings.
Why Choose HICLOVER?
Choosing HICLOVER over trading companies offers significant advantages due to their direct manufacturing expertise and stable supply chain. Their containerized modular systems and PLC automation ensure reliable, efficient waste management solutions. Additionally, the mobile plug-and-play design of their systems supports deployment in remote and challenging environments, such as remote mining or oil camps.
For more information on HICLOVER and their range of waste incinerators, visit their official website [here](www.hiclover.com/) or contact them through their [contact page](hiclover.com/contact/).
Comments are closed